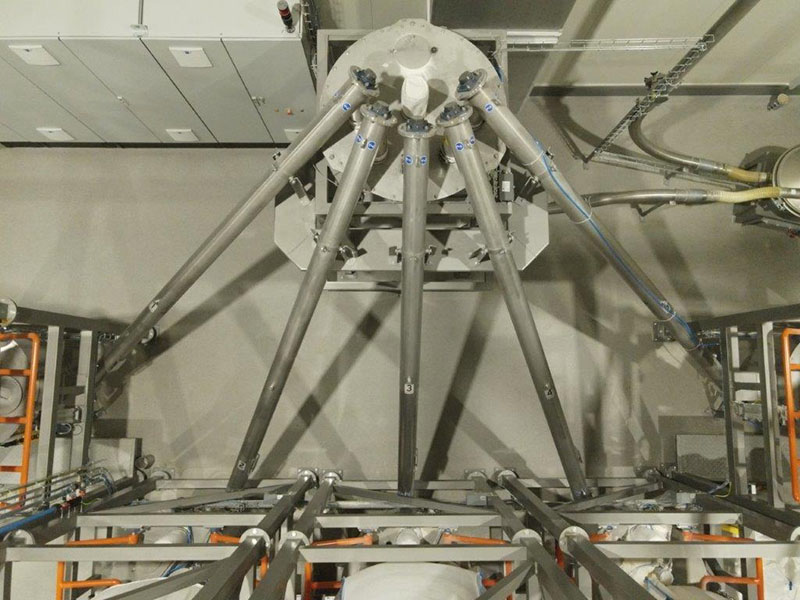
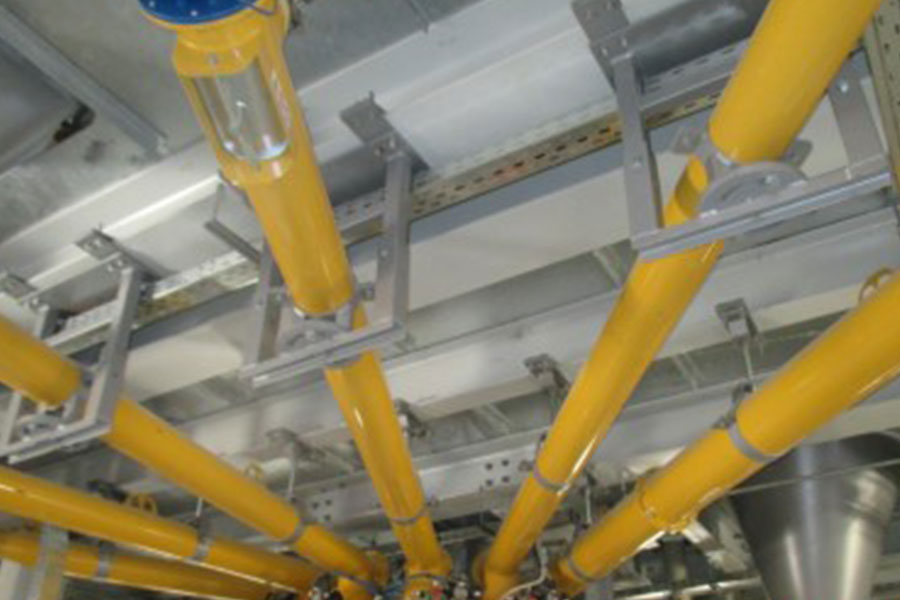
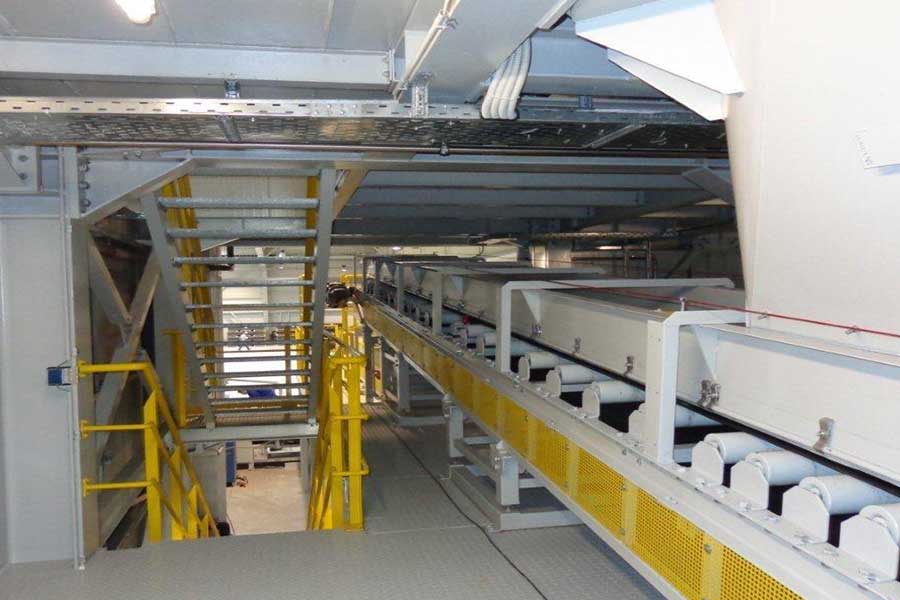
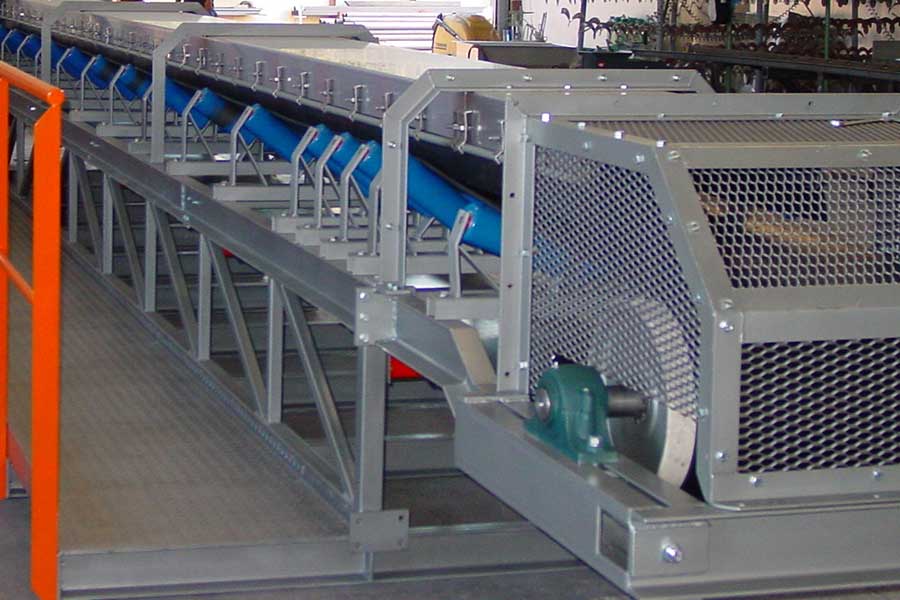
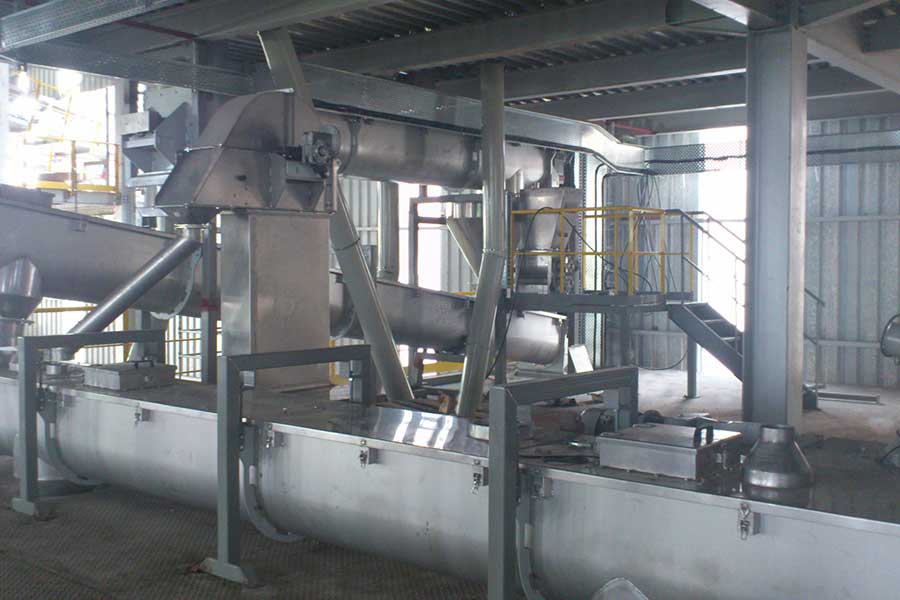
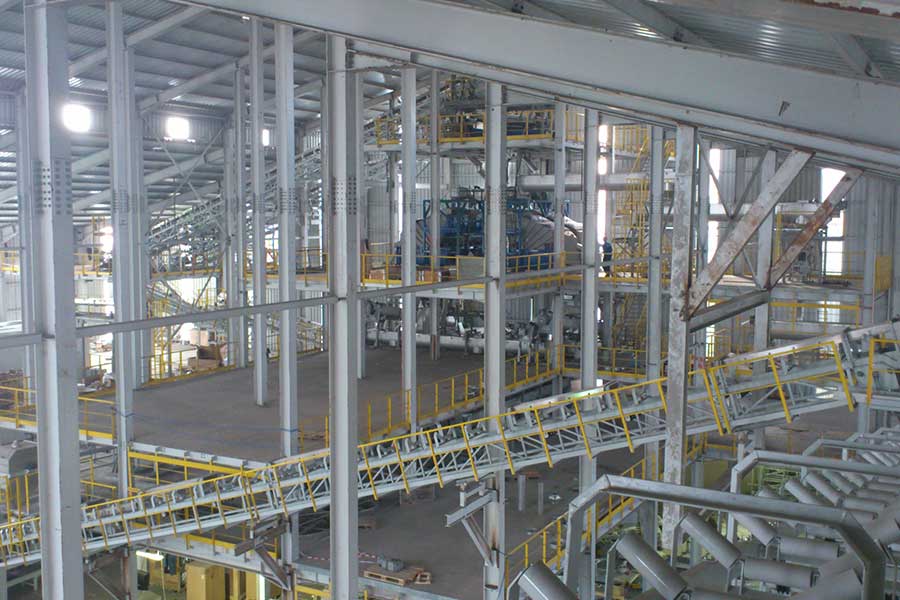
Mechanical conveying includes screw and chain conveyors, bucket elevators, aero-mechanical and tubular drag conveyors, belt conveyors, vibrating and so on, all of which could be manufactured in different types and shapes yet with conveying capacities ranging from few kg/hr to few hundreds tn/hr. Mechanical conveying is usually in place for short distances and is considered a cost effective means of transport comparing with pneumatic ones. Ideally considered also to applications where sensitive seeds or powders need to be conveying.
There is no ‘one fits all’ solution as in many cases even in the same factory, even for the same raw material a different type of conveying is selected simply because another factor comes along to a specific process step.
A proper design put into place right from the start is for great importance to reach a “get it right the first time’’ approach, which saves significant costs in the long run both in efficiency and maintenance while the majority of the cases ends up out of specs or inconsistent final products.